


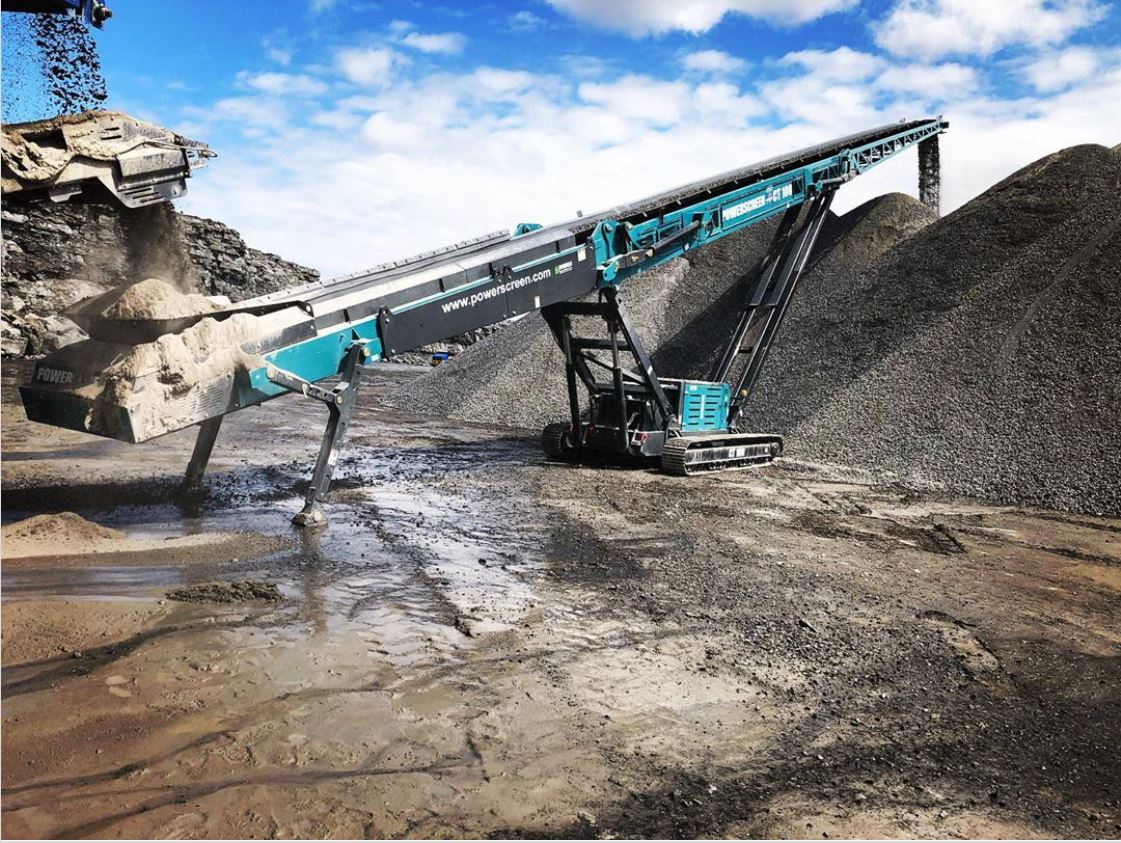
Efficiency, productivity and increased stockpile capacity are just some of the benefits available from ELB Equipment’s latest offering of Powerscreen mobile conveyors.
The latest range of Powerscreen mobile conveyors offers reduced crushing and screening costs with the use of mobile conveyor loading solutions and can replace more costly loading equipment in many applications. The manufacturer has one of the largest ranges of off-the-shelf mobile conveyor systems globally. According to Wakefield Harding, ELB Equipment national sales manager for mining, the range has tracked conveyor mobile machines ranging from 21 to 30m and from 500 to 1000 tons per hour (tph). He further explained that the tracked radial mobile conveyors range from 20 to 24m and 500 to 1000 tph with stockpile capacities of up to 7500 cubic meters at 180 degrees.Large range
He added that fully mobile tracked hopper feeder ranges from 15 to 23m with hopper capacity from four cubes to 10 cubes with a low-level feeder option that can be fed via loader or excavator directly and has a capacity of seven m³. “We also have lattice frame and telescopic conveyors up to 50m.” Wakefield explained“Furthermore, all the mobile conveyors can be run on automated programme as an optional extra. The advantage of this range of Powerscreen mobile conveyors is that they prevent degradation and segregation of materials meaning that it does not separate fines and heavy materials during the stockpiling process and prevents degradation of material as it is stockpiled.
“This is a key feature in ensuring the improvement of material quality. In addition, the pin less deployment feature allows the operator to adjust the stockpile angle “on the fly”, which in turn, reduces downtime and the chances of blockages at the head drum. This also results in the machine having a faster set-up time. The mobile conveyors also help in the reduction of site traffic, labour and because of their robust design, maintenance costs.”
